What It Is
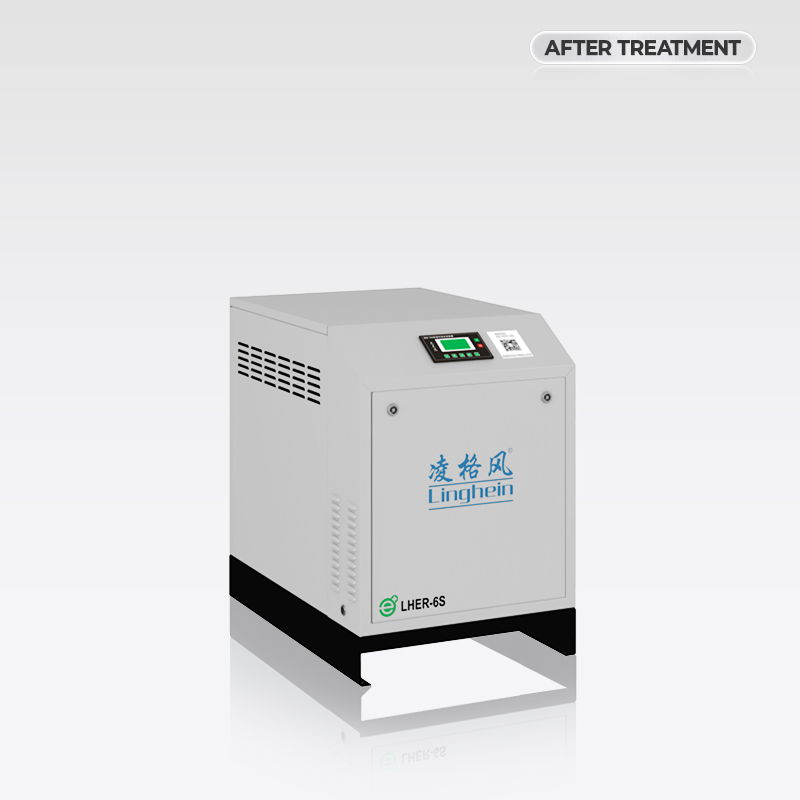
Captures waste heat generated during air compression and converts it into usable thermal energy — hot water for boiler preheating, space heating and sanitary use — lowering both energy costs and carbon footprint
Brand Strength
Wholly owned subsidiary of the Atlas Copco Group member since 2011
Production base in Jiangsu Province; lean manufacturing certified by Lloyd's Register
ISO9001 / ISO14001 / ISO45001 / ISO50001 certified
Global distribution (from 2026) via GASFlow Machinery, with localized service networks and technical support
How It Works
Screw compressors release intense heat during air compression — in standard setups this is simply dissipated by oil coolers, after-coolers, cooling fans or water pumps, wasting energy
Linghein integrates a heavy-duty heat exchanger network into the compressor's oil and air circuits, extracting the heat before it is lost
Features
Premium materials: 316L stainless steel heat exchangers — corrosion-resistant, highly conductive, and fully isolated to prevent oil/water cross-contamination
Fail-safe control: smart thermostatic valve automatically returns oil to standard cooling if hot-water demand drops or flow stops, keeping the compressor in its optimal temperature range
Compact & modular: installs inside the compressor canopy or alongside existing equipment; suited to new machines and retrofits with minimal downtime
Intelligent monitoring: real-time tracking of temperature differentials, flow rates and energy savings for easy ROI measurement
Energy & Sustainability Value
Preheats boiler feed water (e. g., 15°C → 60°C), drastically cutting or eliminating secondary boiler fuel consumption
Thermal energy is fully recovered from an existing process, so the hot water produced is virtually zero-carbon
Cuts emissions, hedges against volatile fuel/electricity prices, and supports carbon-tax compliance and eco-conscious procurement
Industrial Applications
Textile & dyeing — process hot water for washing, chemical preparation, dyeing vats
Food & beverage — container sanitation, CIP cycles, ingredient preheating
Chemical & pharmaceutical — stable, cost-free baseline heating for jacketed reactors and synthesis
Surface treatment & electroplating — heated cleaning, rinsing and plating baths
General manufacturing & automotive — floor heating, worker showers, HVAC air preheating
Global Support GASFlow Machinery
Smooth customs handling, transparent supply chain, prompt worldwide delivery
Custom system schematics, energy-saving projections and installation guidance, co-delivered with Linghein R&D engineers
A proven, Atlas Copco-engineered, internationally certified waste heat recovery system — not just premium hardware, but a strategic upgrade for long-term operational efficiency and sustainability
GASFlow presents the Linghein Heat Recovery, a purpose-built solution that elevates compressed air systems into comprehensive energy management platforms. Designed for industrial environments where efficiency, reliability, and sustainability are paramount, the Linghein Heat Recovery integrates a high-performance compressor core with advanced heat recovery technologies to create a single, compact system that transforms waste heat into useful energy. For manufacturers seeking to optimize operational costs and reduce carbon footprints, this product delivers measurable returns while preserving the robust performance expected from GASFlow’s screw air compressors
Product Overview and Key Features
The Linghein Heat Recovery is a modular heat recovery compressor engineered to meet the demands of modern industrial processes. At its center is a proven rotary screw compressor from GASFlow’s portfolio, optimized to provide steady, oil-free or oil-injected compressed air depending on application requirements
Core features include:
- High-efficiency screw compression unit delivering stable pressure and flow
- Integrated plate or shell-and-tube heat exchangers sized for maximal heat transfer
- Intelligent control interface that prioritizes heat routing, compressor staging, and system diagnostics
- Compact footprint and modularity for ease of installation and retrofit applications
- Robust construction and ISO-certified manufacturing to ensure long-term uptime
These features combine to produce a heat recovery compressor that supports both continuous and intermittent duty cycles while maximizing energy capture
Applications and Use Cases
The Linghein Heat Recovery is ideal for factories, processing plants, food and beverage operations, chemical facilities, and any industrial environment where compressed air is essential. Typical applications include:
- Space heating for workshops and production halls using recovered heat, reducing reliance on fossil-fuel boilers
- Domestic hot water and process water preheating, lowering the energy required for downstream heating systems
- Drying ovens and thermal processors that can utilize steady low-grade heat reclaimed from compression
- Combined heat and power (CHP) augmentations where waste heat from compressed air systems complements other heat sources
By reclaiming heat on-site, facilities can realize significant reductions in primary energy consumption and operational costs, while promoting industrial waste heat reuse that aligns with sustainability goals
Innovation and Technical Advantages
The Linghein Heat Recovery stands out through its combination of compressor expertise and targeted thermal integration. Several technical innovations deliver measurable advantages:
- Intelligent control for dynamic heat allocation: Advanced control algorithms prioritize heat recovery during peak thermal demand and can divert heat to buffer tanks or bypass when storage is full, preserving compressor efficiency and system safety
- Low-temperature differential design: By maintaining efficient heat transfer even at low temperature differentials, the Linghein Heat Recovery maximizes usable heat volume and broadens potential applications for industrial waste heat reuse
- Minimal parasitic losses: The heat recovery compressor minimizes additional pressure drop and motor load, ensuring that energy recovery does not come at the expense of compressed air performance
- Modular design for scale and redundancy: Plants can deploy multiple units in parallel to match capacity and enable staged operation for improved part-load efficiency
Energy and Sustainability Benefits
Incorporating the Linghein Heat Recovery into an energy-efficient air system yields tangible sustainability benefits. A majority of input electrical energy in compressor systems is dissipated as heat; the Linghein Heat Recovery reclaims this energy and converts it into usable thermal output
Installation and Integration
GASFlow designed the Linghein Heat Recovery for straightforward installation in new build and retrofit contexts. The heat recovery compressor unit’s compact arrangement simplifies placement near compressor rooms, enabling shorter piping runs for thermal transfer and reducing installation complexity
Reliability and Serviceability
GASFlow’s dedication to ISO-certified manufacturing and rigorous RD ensures that the Linghein Heat Recovery meets demanding industrial reliability standards. Service access is optimized for routine inspection, filter changes, and heat exchanger maintenance. Local support and global technical backup from GASFlow ensure rapid response for parts and service, safeguarding uptime and preserving the long-term benefits of the energy-efficient air system
Economic Case and Return on Investment
Facilities adopting a Linghein Heat Recovery typically observe a compelling payback profile driven by reduced boiler fuel costs and improved overall energy utilization. The heat recovery compressor system heat recovery compressor a significant share of compression heat, which can offset heating energy requirements throughout seasonal cycles. When financed over the operational life of the compressor, these savings often justify the initial investment and improve total cost of ownership compared to traditional compressor-only installations
Why Choose GASFlow Linghein Heat Recovery
GASFlow brings a decade-spanning heritage of screw air compressor innovation and manufacturing excellence to the Linghein Heat Recovery. Customers benefit from a solution that is more than a compressor: it is a strategic component of an energy-efficient air system aimed at industrial waste heat reuse
The Linghein Heat Recovery is a forward-looking heat recovery compressor that merges the reliability of GASFlow screw compressors with advanced thermal reclamation. For industrial heat recovery compressor operators committed to reducing operational costs, cutting emissions, and maximizing energy utilization, the Linghein Heat Recovery provides a practical, high-performance path toward a more sustainable and energy-efficient air system. Its heat recovery compressor optimized heat transfer, intelligent controls, and modular flexibility make it an indispensable element for facilities seeking to turn compressed air waste heat into productive value
 EN